
Medical Titanium Wire
Medical Titanium Wire for Implant, Instrument and OEM Programs
Medical titanium wire is titanium wire drawn to a medical specification rather than a commercial one: grade, interstitial limits, diameter tolerance, temper and surface condition are all fixed by the part the wire will become. We draw medical grade titanium wire in Baoji from rod rolled in our own mill — the melt and the rolling are ours, not bought in as drawn wire, so the history behind a coil is one we can trace rather than one we take on someone else’s certificate.
Seven specifications are in routine production: commercially pure Grades 1–4 to ASTM F67; Grade 5, Ti-6Al-4V, to ASTM F1472, and its extra-low-interstitial form, Grade 23, to ASTM F136; and Ti-6Al-7Nb to ASTM F1295 / ISO 5832-11. The ASTM specifications named here are all surgical implant material specifications — F67 for unalloyed titanium, F1472 for standard-grade and F136 for ELI wrought Ti-6Al-4V.
Diameters run from Ø0.10 mm to Ø6.0 mm depending on grade and product form, supplied annealed, cold-drawn or stress-relieved, as coils or cut to length. After the grade, the condition is the decision that most often decides whether the wire forms or cracks.
Pick the grade first, the rest follows
Most price arguments are really grade-and-temper arguments. Start here, then match diameter and condition to your forming step.
| Grade | Governing standard | Range (Ø, mm) | Specify it when |
|---|---|---|---|
| Grade 1 CP |
ASTM F67 Gr.1 ISO 5832-2 |
0.10 – 3.0 | The part is non-load-bearing and formability beats strength: suture components, fine instrument parts, micro-springs. |
| Grade 2 CP |
ASTM F67 Gr.2 ISO 5832-2 |
0.20 – 5.0 | You need ductility for bending, looping or twisting: cerclage wire, wire forms, fixation shaped in theatre. |
| Grade 3 CP |
ASTM F67 Gr.3 ISO 5832-2 |
0.30 – 5.0 | A medium-strength unalloyed option is enough: more strength than Grade 2 without going to an alloyed grade. |
| Grade 4 CP |
ASTM F67 Gr.4 ISO 5832-2 |
0.30 – 5.0 | The strongest unalloyed option is specified and the part still has to bend: dental wire, load-bearing CP components. |
|
Grade 5 Ti-6Al-4V |
ASTM F1472 ISO 5832-3 |
0.50 – 6.0 ≥4.76: form agreed |
The drawing names standard-grade Ti-6Al-4V to ASTM F1472 — the wrought implant specification for this alloy — and the design does not call for ELI chemistry. State the product form as well as the size. |
|
Grade 23 Ti-6Al-4V ELI |
ASTM F136 ISO 5832-3 |
0.30 – 5.0 | The design calls for ELI chemistry — lower oxygen and iron — because the section is fatigue-critical, or the device file already names F136. |
|
Ti-6Al-7Nb Nb-stabilised, V-free |
ASTM F1295 ISO 5832-11 |
0.50 – 5.0 | The program rules out vanadium, or the hospital specification already names this alloy. |
Grade 5 and Grade 23 are both Ti-6Al-4V, but not the same material on a purchase order. Both ASTM F1472 and ASTM F136 are surgical implant material specifications for wrought Ti-6Al-4V; the difference is that F136 specifies the extra-low-interstitial chemistry, so the two carry different limits and, in places, different acceptance values. Oxygen and iron are quoted here because they are the items that separate the two grades — 0.20% O and 0.30% Fe permitted under F1472 against 0.13% and 0.25% under F136 — and not because they are the whole chemistry requirement: both standards also limit aluminium, vanadium, carbon, nitrogen, hydrogen and other elements, and the complete table in the edition your drawing cites is what governs. ELI chemistry is specified where the design wants the better ductility and fracture toughness that follow from the lower interstitials. Neither grade substitutes for the other silently: put the grade, the standard with its edition, the product form and the delivery condition on the drawing and on the purchase order.
Ranges above are what we can supply per grade, not an order grid: the envelope across all seven is Ø0.10 – 6.0 mm, each ceiling is set by how that alloy draws, and for Grade 5 the top of the range is fixed by the product form as much as by the diameter. Anything outside a range is a conversation — raise it before the drawing is frozen.
At the top of the Grade 5 range the product form has to be agreed rather than assumed. Most wrought titanium specifications put the wire/bar line at 4.76 mm (3/16 in.), and ASTM F1472 states its mechanical requirements by product form and size rather than as one value for the alloy — so a 5 or 6 mm order is not automatically “F1472 wire”. Tell us which form you want with the size; we confirm the standard, the acceptance values for that form and the certificate basis in writing before the order is placed.
Send grade, governing standard, diameter with its tolerance, temper, surface and length. We confirm what we can hold before you raise a purchase order — and say so if we cannot.
Seven grades, three series
All three are medical titanium wire to a named standard; what changes between them is the alloy system and the standard behind it, not the drawing discipline. If the grade is already fixed by the design file, start with the series it belongs to.
Non-load-bearing parts and anything shaped in theatre. Soft-drawn where the wire has to be formed, annealed where it has to survive a bend without a springback argument.
Ø0.50–6.0 mm
Grade 23 (ELI) · ASTM F136
Ø0.30–5.0 mm
Where CP is not strong enough. Both grades are implant material; which one your part needs is decided by the chemistry the drawing calls up, not by the alloy name.
Ø0.50–5.0 mm
Vanadium-free, for programs that rule V out or where the hospital specification already names the alloy.

The Four Fields on Your Drawing That Decide the Wire You Receive
Grade and diameter get written down; temper, tolerance, surface and format often do not. That is where a wire order quietly fails — the coil meets its certificate, and the part still cracks at the heading station. Here is what each field controls.
| Field | What we supply | Why it decides your process |
|---|---|---|
| Diameter and tolerance | Ø0.10 – 6.0 mm across the grades tabulated above; step size and tolerance band confirmed per order, in writing, before the PO. | Half a tolerance band decides whether a 0.2 mm wire feeds through your straightener or jams it. Fix the band before the price. |
| Temper and condition | Annealed for maximum elongation, cold-drawn for tensile and spring-back, or drawn then stress-relieved. | Forming, coiling and heading want soft wire; archwires, K-wires and elastic devices want spring temper. One grade, two materials. |
| Surface finish | Drawn, pickled, polished or fine-polished. Surface is checked by optical inspection rather than by eye; the inspection plan for your order is agreed at quotation. | Draw marks and residual oxide become crack starters in fatigue parts, and contamination in implant cleaning lines. |
| Delivery format | Coils for continuous feed; straight lengths cut to a fixed length for CNC or hand assembly. | Straight lengths cost more per kilo, but remove a straightening step and a scrap source from your line. |
Ranges move with the alloy, not with convenience: Grade 2 stops at Ø5.0 mm while Grade 5 runs to Ø6.0 mm — with the product form confirmed above 4.76 mm. If the design needs commercially pure titanium at 5.5 mm, raise it early: the answer depends on the grade, not on the diameter.
Mechanical Property Minimums by Grade and Condition
The figures below are the minimums the cited specifications write for the forms they cover, not marketing targets — what a certificate should show and what your model should assume. The comparison is drawn on annealed material, the condition in which these grades are most often specified; it is not a claim that every one of these standards tabulates only the annealed condition, and where a standard also carries cold-worked or other conditions, those values are not reproduced here.
| Grade | Standard | Condition | Tensile (MPa) | Yield (MPa) | Elongation (%) |
|---|---|---|---|---|---|
| Grade 1 CP | ASTM F67 Gr.1 | Annealed | ≥ 240 | ≥ 138 | ≥ 24 |
| Grade 2 CP | ASTM F67 Gr.2 | Annealed | ≥ 345 | ≥ 275 | ≥ 20 |
| Grade 3 CP | ASTM F67 Gr.3 | Annealed | ≥ 450 | ≥ 380 | ≥ 18 |
| Grade 4 CP | ASTM F67 Gr.4 | Annealed | ≥ 550 | ≥ 485 | ≥ 15 |
|
Grade 5 Ti-6Al-4V |
ASTM F1472 |
Annealed bar / forging reference † |
≥ 930 | ≥ 860 | ≥ 10 |
|
Grade 23 Ti-6Al-4V ELI |
ASTM F136 | Annealed | ≥ 860 | ≥ 795 | ≥ 10 |
|
Ti-6Al-7Nb Nb-stabilised |
ASTM F1295 | Annealed | ≥ 900 | ≥ 800 | ≥ 10 |
*Floors, not targets — and on three points a table like this cannot settle the answer for you. Grade 1 yield reads 138 MPa because that is where ASTM F67 puts it; ISO 5832-2 puts the same grade at 170 MPa, so name the standard and the edition your design file is written against. † The Grade 5 line is the bar and forging minimum from ASTM F1472, reproduced as a reference for the alloy rather than as an acceptance value for wire. F1472 states its mechanical requirements by product form and size, and wrought titanium specifications normally put the wire/bar line at 4.76 mm, so the values that apply to your order are the ones for the form on your drawing, and the certificate states which. And cold-drawn or stress-relieved wire has no value in this table at all; temper and tensile are agreed against your forming step.
Meeting a material specification is a statement about the material, not about the device made from it. Biocompatibility, fatigue life, corrosion behaviour and sterilisation performance are established by testing on the finished device, under the regulatory route that applies to it — a certificate to F67, F136 or F1472 does not stand in for that work.
What “Ultra Clean” Should Mean in Your Specification
No standard defines “ultra clean”. When a buyer asks for ultra clean titanium wire, the phrase is usually standing in for one of four different requirements — and two suppliers can both promise it while shipping very different coils:
- Low interstitial content. Oxygen, nitrogen, hydrogen and carbon held at the low end of the grade range — the gap between standard Grade 5 and ELI, and one of the variables behind how a wire behaves at a tight bend radius.
- No embedded contamination. Oxide scale and drawing lubricant removed before passivation rather than wiped off, which is what resurfaces as inclusions or staining after sterilisation.
- No surface defects. No seams, folds or draw lines that act as fatigue initiation sites on a 0.3 mm section.
- A batch you can point back to. Chemistry, mechanical results and inspection records tied to one melt and one coil — otherwise cleanliness cannot be verified after delivery.
A quotation that says “ultra clean” without naming which of these four it controls, and how it measures them, is using the word as decoration. Ours is described in the next section; which of the checks apply to a given order is agreed at quotation, in writing.
From Ingot to Coil: How Medical Titanium Wire Is Made and Checked
Melting and rolling are not outsourced
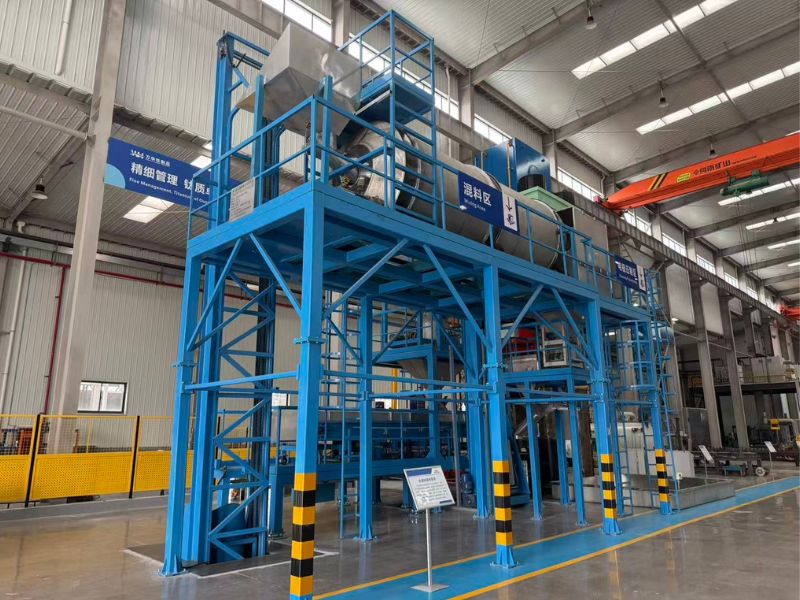
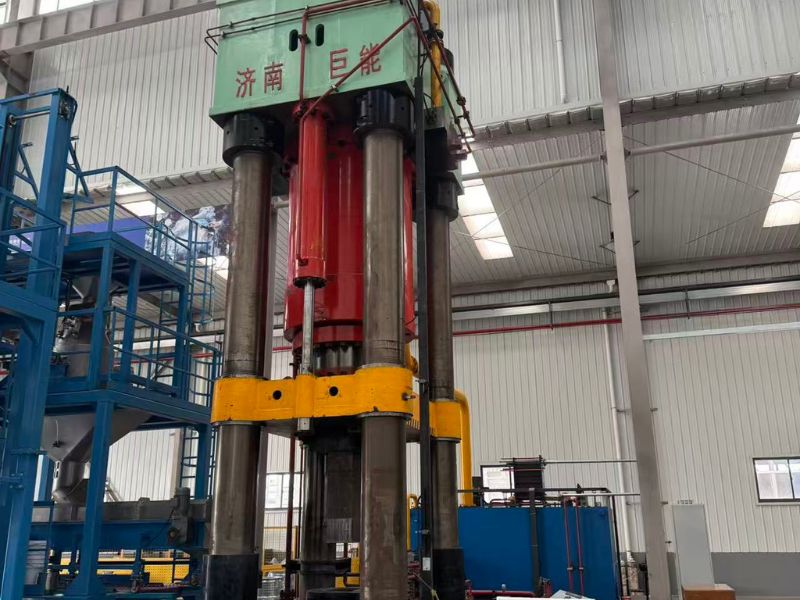
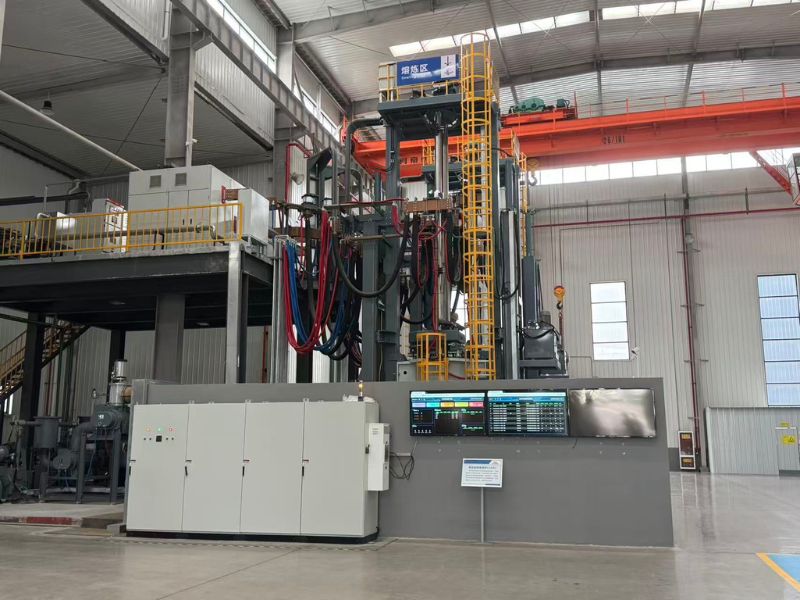
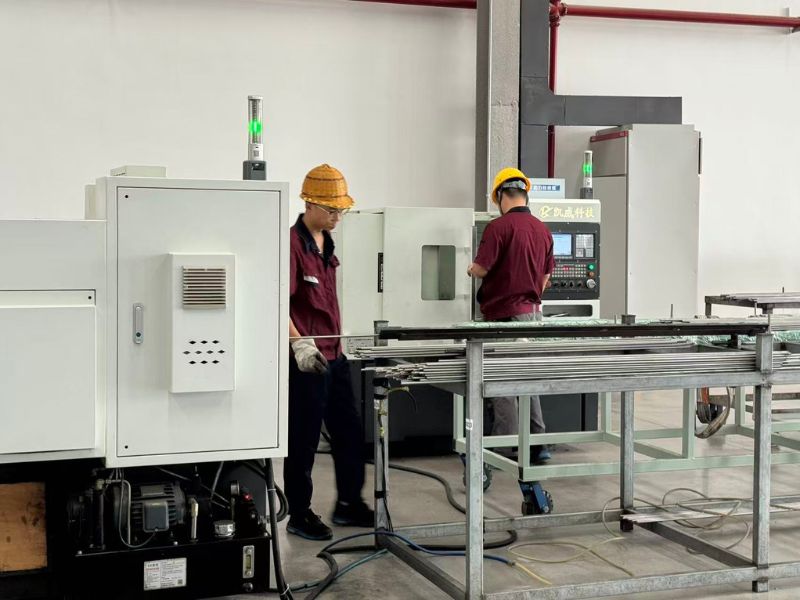
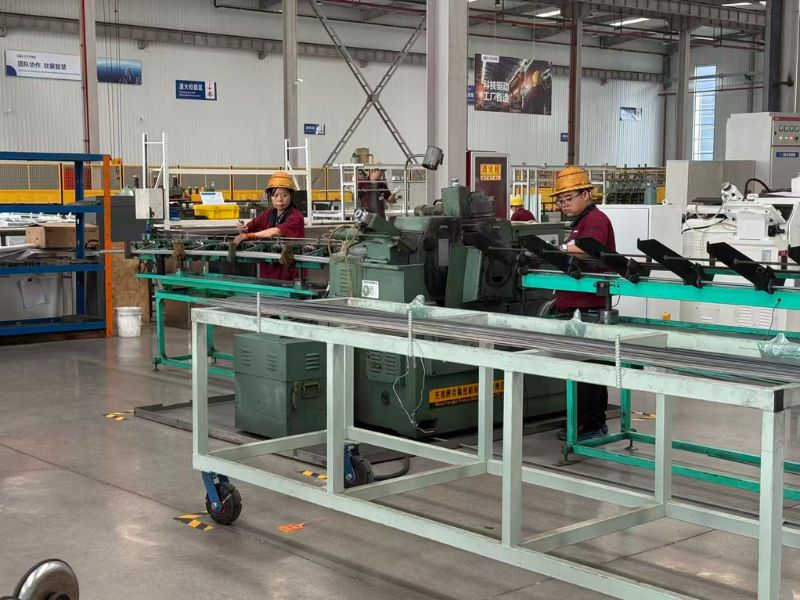
Wire quality is settled before the drawing die: in the sponge, the melt and the rod. We start from 0A-grade titanium sponge, melt three times in vacuum arc furnaces, and roll rod in our own mill instead of buying drawn wire from a third party. What that buys you is a known history instead of an assumed one — it does not buy a fixed lead time, which depends on grade, diameter and temper and is quoted alongside the price.
What is checked, and what is agreed per order
- Chemistry — analysed against the limits of the grade and the edition named on the drawing, before drawing begins.
- Mechanical properties — tensile, yield and elongation reported for the lot supplied; the sampling frequency for your order is stated in the quotation and repeated on the certificate.
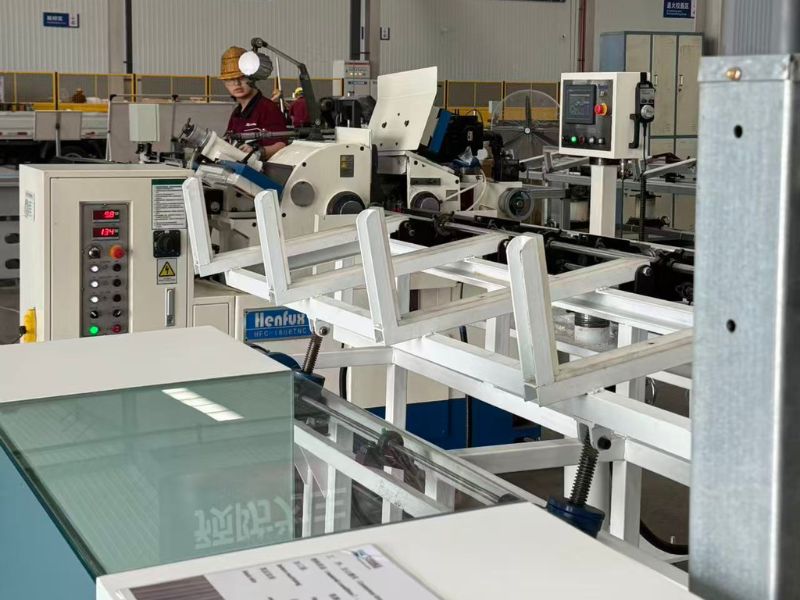
- Ultrasonic inspection — automatic rotary-head testing of bar and rod, upstream of drawing.
- Dimensional and surface — diameter and surface checked by optical inspection rather than by eye; how much of that happens in process and how much at final inspection is agreed per order.
- Metallography — structure examined where the application is fatigue-critical. Ask for it and it is quoted as an added test rather than assumed.
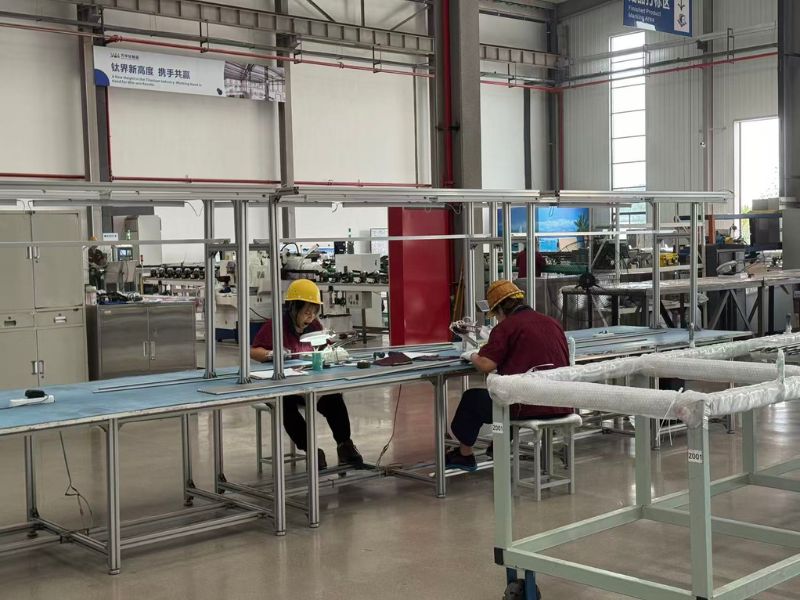
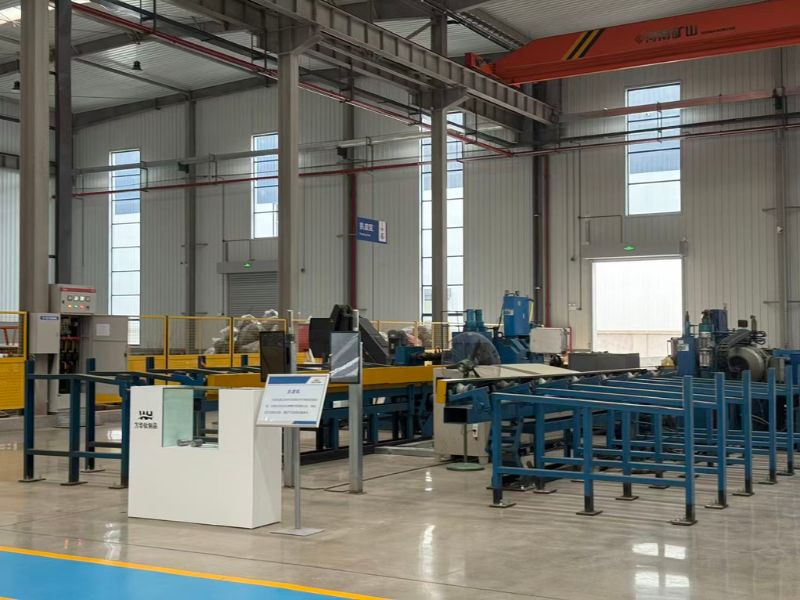
Quality is a nine-person function, about 15% of the company, responsible for inspection and for the documentation that travels with each lot. The system is certified to ISO 9001:2015. Where a device maker needs ISO 13485-linked documentation — a quality agreement, a process description for the technical file, a declaration of conformity to a named edition — tell us at RFQ and we confirm what we can issue, in writing, before the order. More on the plant and its melting and processing chain, or on how the material behaves in biocompatibility testing.
Where Medical Titanium Wire Is Used
Four application families account for most of what we ship. Each pulls a different combination of grade, temper and surface, so one diameter can be two different products:
- Orthopedic fixation — cerclage and tension-band wire, K-wires, elastic intramedullary nails. Soft-drawn CP for shaping in theatre, alloy where the section or the device file calls for it — the grade table above sets out which. See highly elastic titanium wire for Kirschner wires and IM nails.
- Dental — archwire, abutment and framework components, orthodontic accessories, where fine diameter and dimensional control are the whole specification.
- Surgical instruments — springs, forceps tips and reusable micro-tools that see repeated sterilisation, where corrosion resistance and cleanability are part of the specification.
- Cardiovascular and interventional — guidewire cores and delivery components, where cleanliness and consistency outrank strength.
If the part is machined from solid rather than formed from wire, wire is the wrong input — look at medical titanium bar or sheet and plate. The bar, sheet or wire comparison covers how to make that call.
Send Seven Details, Get a Wire Quotation
A quotation for medical titanium wire only helps if it matches what your line can run. Give us these seven fields and the reply is a specification confirmation instead of a price list:
- Grade — “Grade 23”, not simply “medical titanium”.
- Governing standard — ASTM F136, F1472 or F67, or the ISO 5832 part, with the edition your device file cites.
- Diameter — the nominal size, plus the product form, which starts to matter from 4.76 mm up.
- Tolerance band — a nominal size alone is not enough on fine wire.
- Temper or condition — annealed, cold-drawn or stress-relieved.
- Surface finish — drawn, pickled, polished or fine-polished.
- Delivery form and quantity — coil or straight length, with the weight or metres per delivery.
Lead time depends on grade, diameter, temper and whether the size is in routine production, so it is quoted with the price rather than after it. Documentation scope — what the certificate states, any added test, any declaration your device file needs — is settled in the same reply, so nothing about the paperwork is left until after the order.
The form opens over this page — no redirect. Paste the seven fields into the message box and we reply with a specification confirmation.
Wire Sourcing Questions Engineers Ask Us
Not automatically — and “implant grade” is not a synonym for Grade 23. What makes material implant grade is the specification it is certified to and the traceability behind the certificate. ASTM F67 covers unalloyed titanium for surgical implants, ASTM F1472 covers wrought standard-grade Ti-6Al-4V for surgical implant applications, and ASTM F136 covers the ELI version of the same alloy for the same purpose: all three are implant material specifications, and which one is right follows from the device, not from the adjective. “Medical grade” is the looser term — material intended for medical manufacturing and certified to a medical specification, without saying which. Ask for the standard and its edition, and say whether the part is implanted: that is what decides between F67 Grade 2, F1472 Grade 5 and F136 Grade 23.
Whichever your device file names, quoted with its edition. F67 is the unalloyed titanium specification for surgical implants, F1472 the standard-grade wrought Ti-6Al-4V specification and F136 the ELI Ti-6Al-4V specification — all three written for implant applications. ISO 5832-2, -3 and -11 are the ISO material standards for the same three material families. They are corresponding standards rather than identical documents: editions, test methods and some acceptance values differ, so an ASTM certificate does not automatically satisfy an ISO citation. Check the edition and the acceptance requirements your file calls up, and where it cites both, say which one governs. The failure mode to avoid is not a wrong alloy but a certificate issued to a different standard than the drawing names.
The band that holds depends on grade, diameter, temper and how the wire is handled after it leaves us, so there is no single number that applies across that range. What we will not do is quote a band we cannot verify. Tell us the functional requirement — what the wire feeds through, or what the finished part has to hold — and we propose the widest band that still works: often cheaper than the number already on the drawing, and easier to hold.
All three: annealed, cold-drawn and stress-relieved. Temper and diameter are not independent — the cold reduction that suits one diameter and forming step will not suit another, and the same temper name can behave differently at 0.2 mm and at 1.0 mm. Describe the forming step — heading, coiling, bend radius — and we agree the condition against it rather than against a temper label.
An MTC for this material normally states the heat number, grade and governing standard, the chemical analysis against the specified limits, tensile, yield and elongation results, dimensions and surface condition, and the tests performed. What is agreed per order is the granularity and the extras: whether results are reported per heat or per lot, whether an additional test or a witnessed inspection is included, and whether you need a declaration of conformity to a named edition. That scope is fixed at quotation and repeated on the certificate for the lot. We do not issue a certificate for a test we did not run.
We melt and roll the rod ourselves and draw in-house, so the 0A-sponge input and the triple-melt history are known to us rather than assumed from a supplier’s certificate. It also keeps a non-standard diameter or temper inside one chain of custody instead of splitting it between two companies.